言語

見積もりを取得します
見積もりを取得します
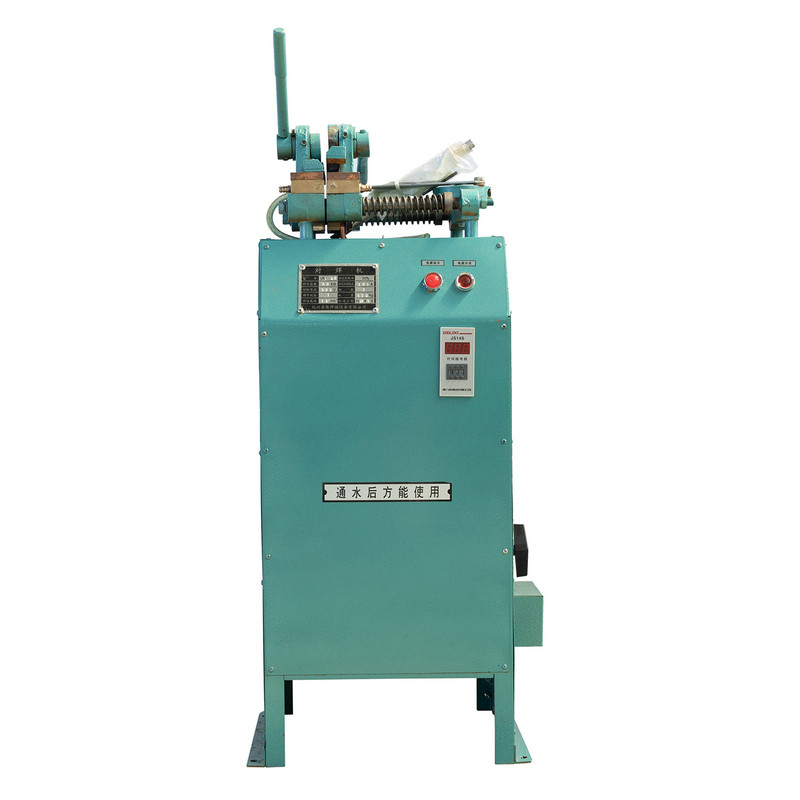


UN1-1KWメタルシェルハンド操作バット溶接機には、主に溶接変圧器、固定電極、可動電極(クランプ)、加圧フィーディング機械、制御成分が含まれています。溶接機は、さまざまな産業で、低炭素鋼、非鉄金属(銅、アルミニウム、銅 - アルミニウム合金)に高品質のバット溶接を行うことができます。メインスイッチ回路はACコンタクタによって制御され、溶接性能が安定して信頼性を高めます。メンテナンスが簡単です。

仕様
| モデル | ユニット | Un1-1KW | |
| 一次電圧 | v | 220 | |
| 定格容量 | Kva | 1 | |
| 評価された一次電流 | A | 4.5 | |
| 定格負荷期間 | % | 8 | |
| 負荷電圧はありません | V | 0.65-2.0 | |
| 二次電圧調節段階 | ステージ | 8 | |
| 最大の動揺力 | N | 10 | |
| 最大給餌ストローク | mm | 3 | |
| 最大顎距離 | mm | 7 | |
| 最大溶接直径 | 低炭素鋼 | mm | 0.6-2.0 |
| 銅 | mm | 0.6-1.6 | |
| アルミニウム | mm | 0.6-1.6 | |
連絡を取り合う

すべての溶接は製造上の決定です。電気溶接機を選択するときは、溶接の品質、サイクル タイム、現場でのオペレータの労力のバランスを取る方法を選択することになります。抵抗溶接装置を何年も構築してきた私たちは、同じパターンを目にしてきました。最初に材料の厚さ、毎日の生産量、電極の予算を定義した購入者が、最終的には自費で支払える機械を購入することになります。このステップをスキップした購入者は、多...
続きを読む
Understanding Resistance Butt Welding and the Role of Flash Weld Technology Joining two metal bar ends face to face without filler material is one of the oldest challenges in metal fabrica...
続きを読む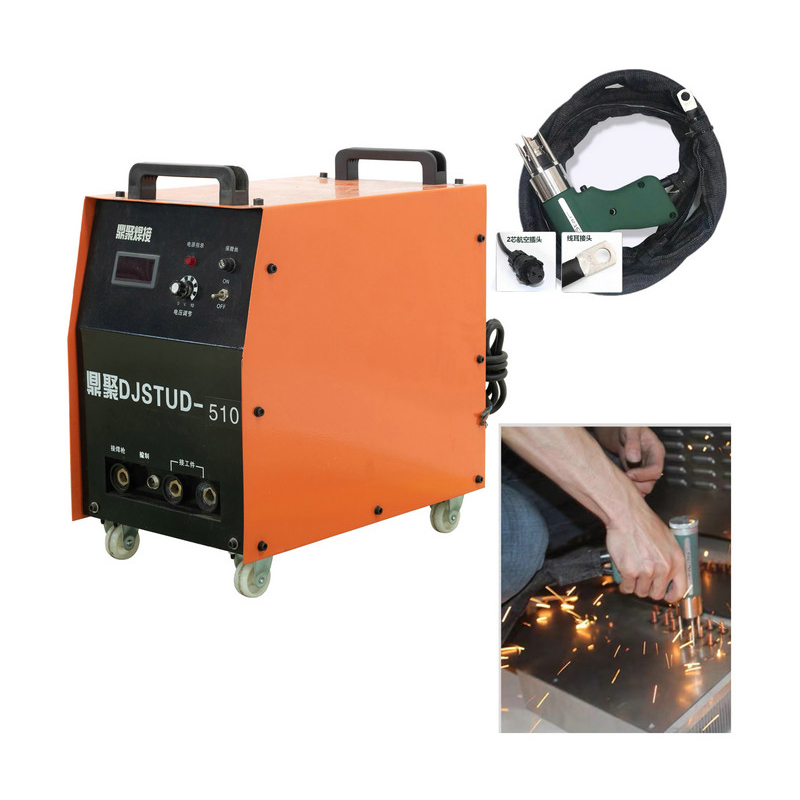
Understanding Stud Spot Welding Technology Today Fastening components to metal panels without drilling or riveting has become a standard requirement across sheet metal fabrication, shipbui...
続きを読む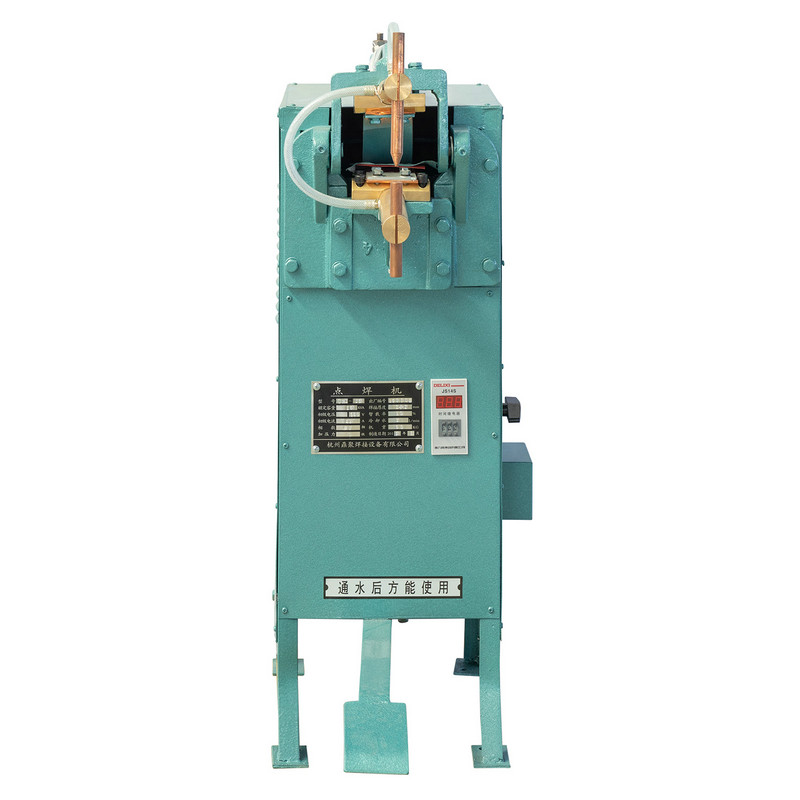
Spot Welding Machine Categories and How They Differ Resistance spot welding equipment is generally divided by how the electrode force is generated and applied. Mechanical foot-pedal units ...
続きを読む
Why Heat Is the Hidden Bottleneck in Spot Welding すべての抵抗スポット溶接は、本質的には制御された熱イベントです。短時間の強力な電流パルスが 2 枚の重なり合った金属シートを通過し、その界面の抵抗によって十分な熱が発生し、それらを瞬時に融合させます。オペレータがめったに考えないのは、溶接が行われた後にその熱がどこに行くかとい...
続きを読む
Why Electrode and Controller Maintenance Determines Weld Quality In resistance spot welding, the quality of every joint depends on two components working in sync: the electrode that delive...
続きを読む
製品
連絡先情報
+86-152-5712-5882
Fax: +86-563-2269966
No. 21 Guangping Road、Guangde Economic Development Zone、Guangde City、Anhui州
QRコード